From alloy melting to precision wire — full in-house control
Nine controlled operations. Every batch traceable to furnace origin. φ0.025mm to 5.0mm capability.
- 01
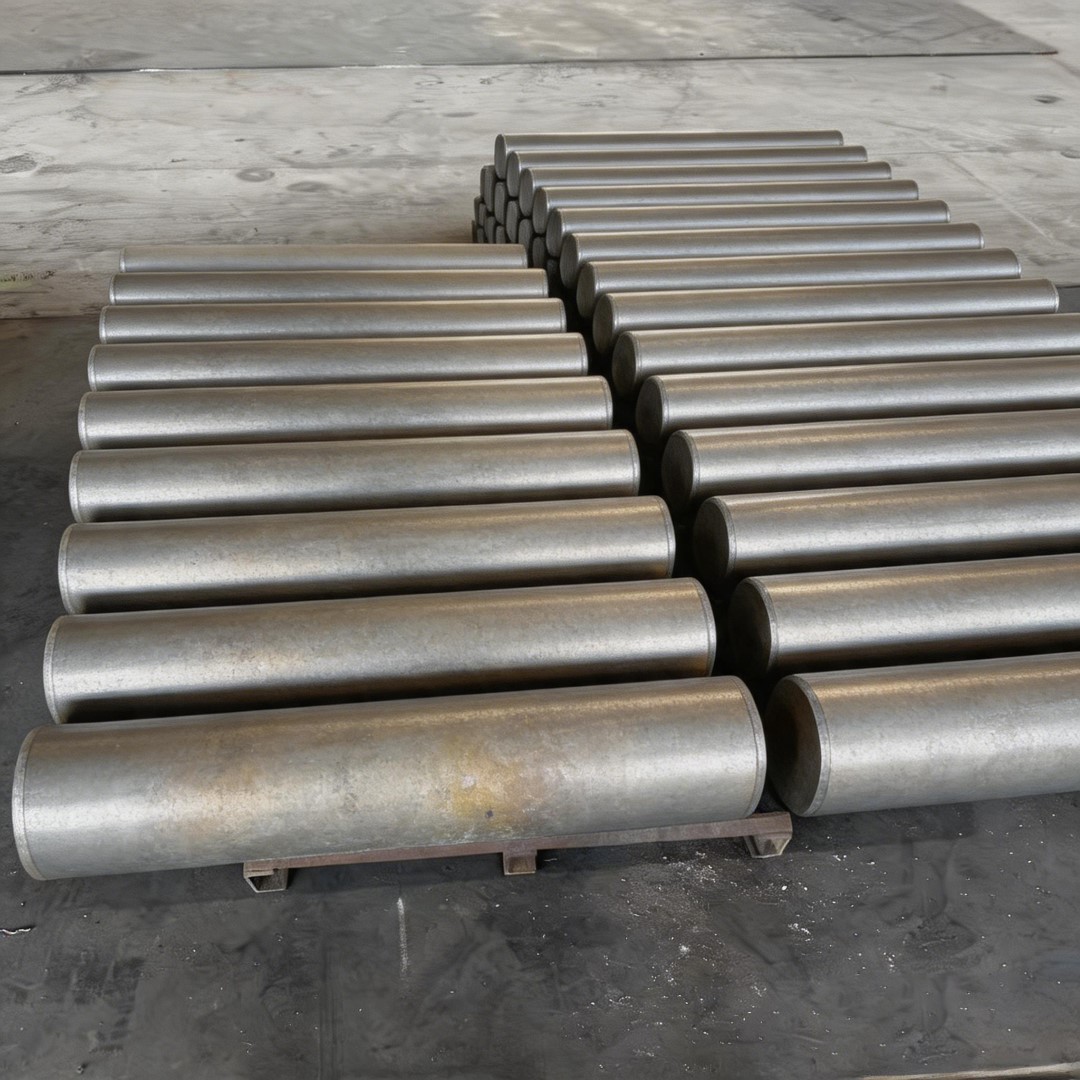
Alloy Melting
Sellable form — Alloy Ingot
Vacuum induction melting holds composition within ±0.1% of specification. Every melt receives a unique furnace number.
VIM furnace · 500 kg
- 02
Hot Rolling
Sellable form — Wire Rod / Billet
Billet reduction to wire rod with controlled temperature and reduction ratio for optimal grain structure.
Continuous mill · φ5.5 mm rod
- 03
Cold Drawing
Sellable form — Cold Drawn Wire (hard)
Multi-pass reduction through tungsten carbide dies, 15–25% reduction per pass.
Multi-block line · 13 passes
- 04
Intermediate Annealing
Sellable form — Annealed Wire (soft)
Hydrogen / nitrogen atmosphere annealing between passes restores ductility and relieves work hardening.
Strand anneal · H2/N2
- 05
Precision Drawing
Sellable form — Ultra-fine Bare Wire φ0.025 mm
Final drawing through single-crystal diamond dies down to φ0.025 mm at ±0.005 mm tolerance.
Diamond die bench
- 06
Final Annealing
Sellable form — Finished Thermocouple Wire
Bright anneal in protective atmosphere for a consistent Seebeck coefficient along the full length.
Inline tension control
- 07
Surface Treatment
Sellable form — Treated Wire
Bright, oxidized or electro-polished finish; surface verified at 40× magnification.
Electro-polishing cell
- 08
100% Testing
Sellable form — Certified Wire
In-line eddy current defect detection, resistance uniformity per spool, laser dimensional verification.
Eddy current + laser micrometer
- 09
Packaging
Sellable form — Packaged Wire
DIN 125 / 160 / 250 spools, coils or custom reels. Batch number engraved, protected for ocean freight.
Automated spooling
Beyond standard requirements
Electrical Testing
- Resistance uniformity per spool (4-wire Kelvin method)
- EMF calibration against reference junction per batch
- Insulation resistance for extension wire
Mechanical Testing
- Tensile strength and elongation
- Surface quality at 40× magnification
- Diameter tolerance by laser micrometer
Traceability System
- Unique furnace number per batch
- Full chemical composition report
- Test data archived 10 years · SGS / BV inspection available
Vacuum Induction Melting Furnace
500 kg capacity
Multi-Pass Wire Drawing Machine
12-die continuous
Controlled Atmosphere Annealing Line
H2 / N2 strand anneal
Eddy Current & Laser Inspection
In-line, 100% coverage
Alloy Melting & Casting
Vacuum induction melting (VIM) for precise thermocouple alloy composition control. Every melt receives a unique furnace number.
Read →Precision Wire Drawing
Multi-pass cold drawing through tungsten carbide and single-crystal diamond dies. From φ5.5 mm hot-rolled rod down to φ0.025 mm.
Read →Quality Control — 100% Testing
Electrical, dimensional and surface inspection on every spool. Test data archived and retrievable by furnace number.
Read →Custom Thermocouple Alloy Orders
Special alloy formulations, non-standard diameters, private labelling and contract manufacturing.
Read →- Custom alloy formulations and sample melts
- Non-standard diameters and tolerance classes
- Special surface finishes
- Custom spool sizes and packaging
- Private labeling and custom part numbering
- Dual certification (IEC + ASTM on the same batch)
Have a custom requirement?
Talk to our metallurgy team about alloy development, contract drawing and dual-certified batches.